Precision laser welding services
Accurate, repeatable laser welds for critical devices and assemblies. We weld in fixtured, automated systems using Swiss-made LASAG lasers with pulse shaping: spots down to 0.0007″, penetration up to 3 mm and helium-tight seams. Hermetic, micro and dissimilar-metal welds for aerospace, medical and defense parts, made in California and shipped across the USA.
Automated welding for repeatable seams
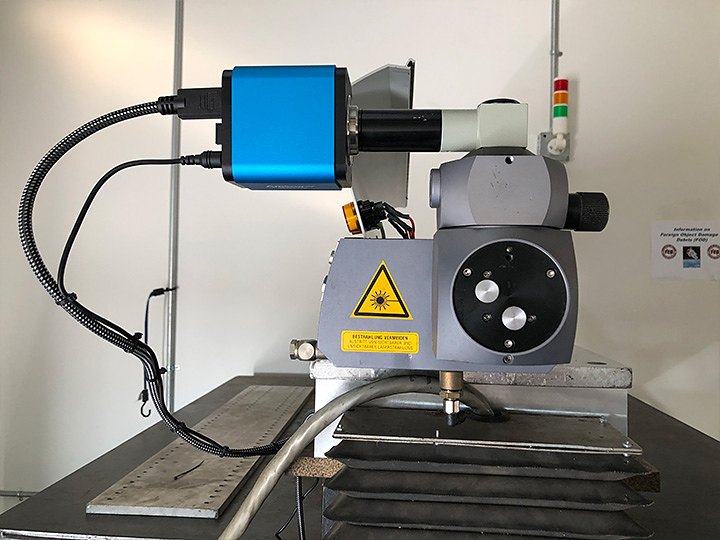
Parts are mounted in a rotary chuck and welded under a motion-controlled laser head with camera alignment. Every part gets the same seam, which suits round housings, caps and feedthroughs.
| Part envelope | Up to 24″ × 30″ |
|---|---|
| Round parts | Up to 18″ diameter |
| Smallest spot | 0.0007″ diameter |
| Weld diameters | 25–1000 µm (SLS 200); spot welds ≥ 40 µm (FLS) |
| Penetration | Up to 3 mm |
| Seal quality | Helium- and pressure-tight welds |
| Laser sources | LASAG (Switzerland), pulse-shaped beam |
| Materials | All metals and many material combinations |
Built to reach larger and multiple parts
The weld head rides an overhead gantry that covers the whole granite work table. It can move across the table, raise and lower, and tilt, reaching all three corners. That means we can weld large parts, several parts in one setup, and seams at awkward angles.
Full-table reach
The head travels the length and width of the table, so big weldments don’t have to be repositioned between seams.
Several fixtures, one setup
Parts can be fixtured at different points on the table and welded in a single run.
Tilting head + rotary axis
The head angles toward the joint while the part turns, for 360° seams on round parts.
- Travels across the full table on the gantry
- Raises and lowers to each position
- Tilts the head for angled and side seams
- Rotary axis for 360° seams
A full 360° seam, the same on every part
For round parts like housings, caps, tubes, valves and feedthroughs, the part turns in the chuck while the beam stays fixed on the joint. Our automated circumferential welding reaches spot sizes as small as 0.0007″, and the built-in microscope camera lets us watch the seam form. The result is one continuous, evenly overlapped seam around the whole circumference, which is what hermetic and pressure-tight parts need.
- Continuous seams around the full diameter
- Even pulse overlap, start to finish
- Angled head for seams on chamfers and shoulders
- Round parts up to Ø 18″
From the Laseronics gallery
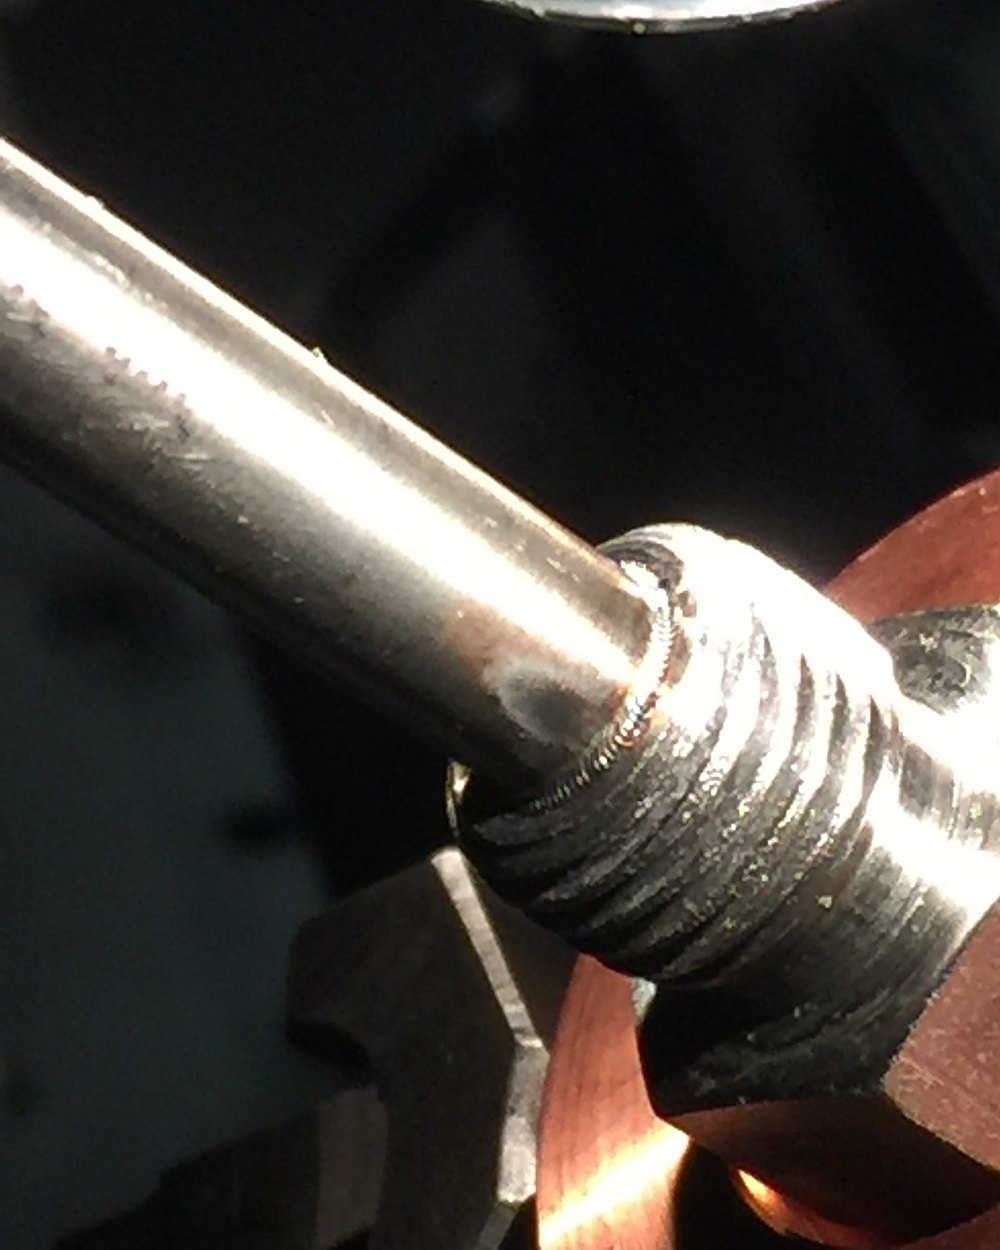
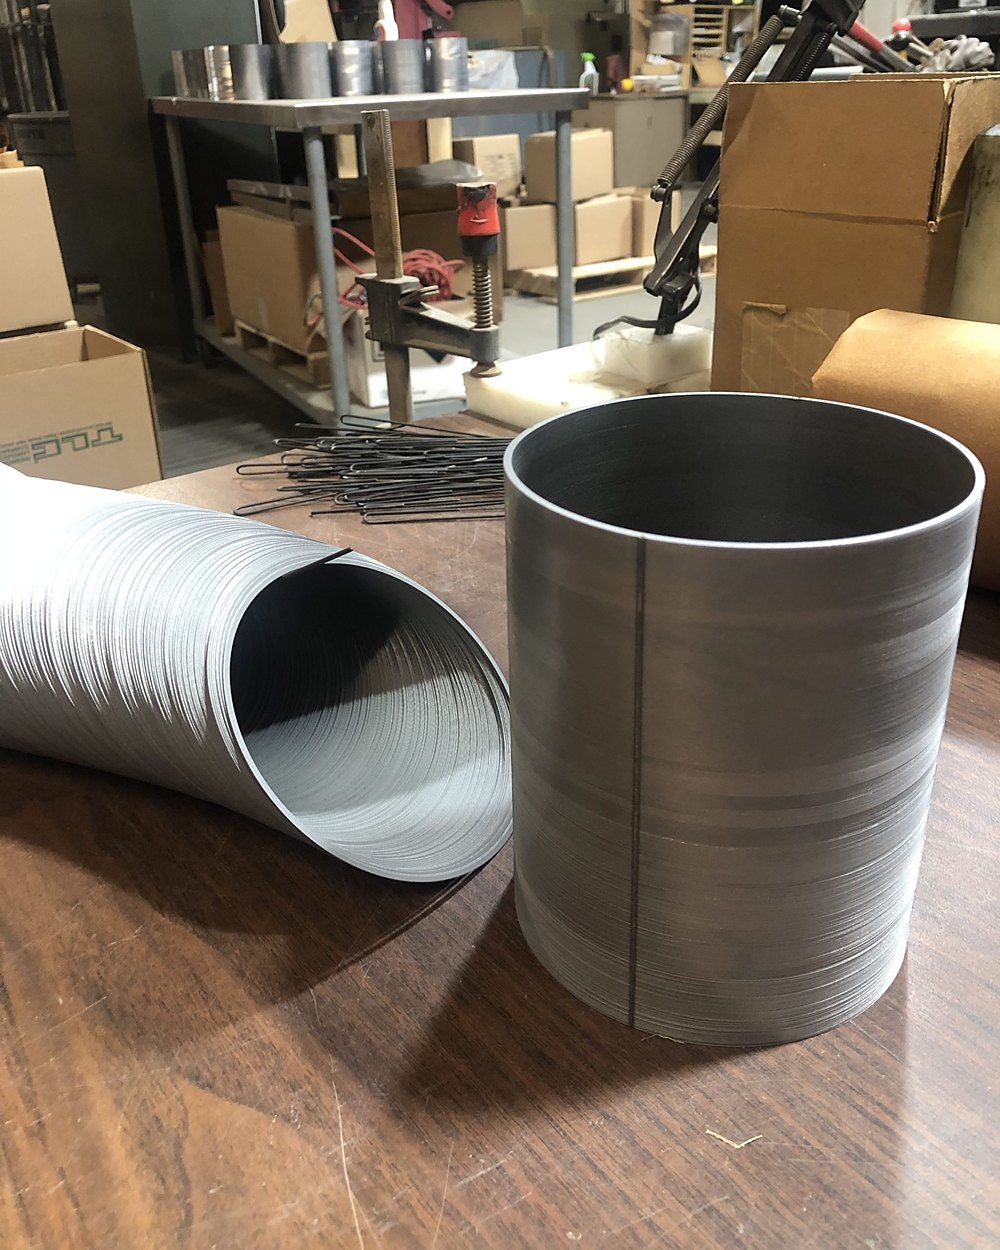
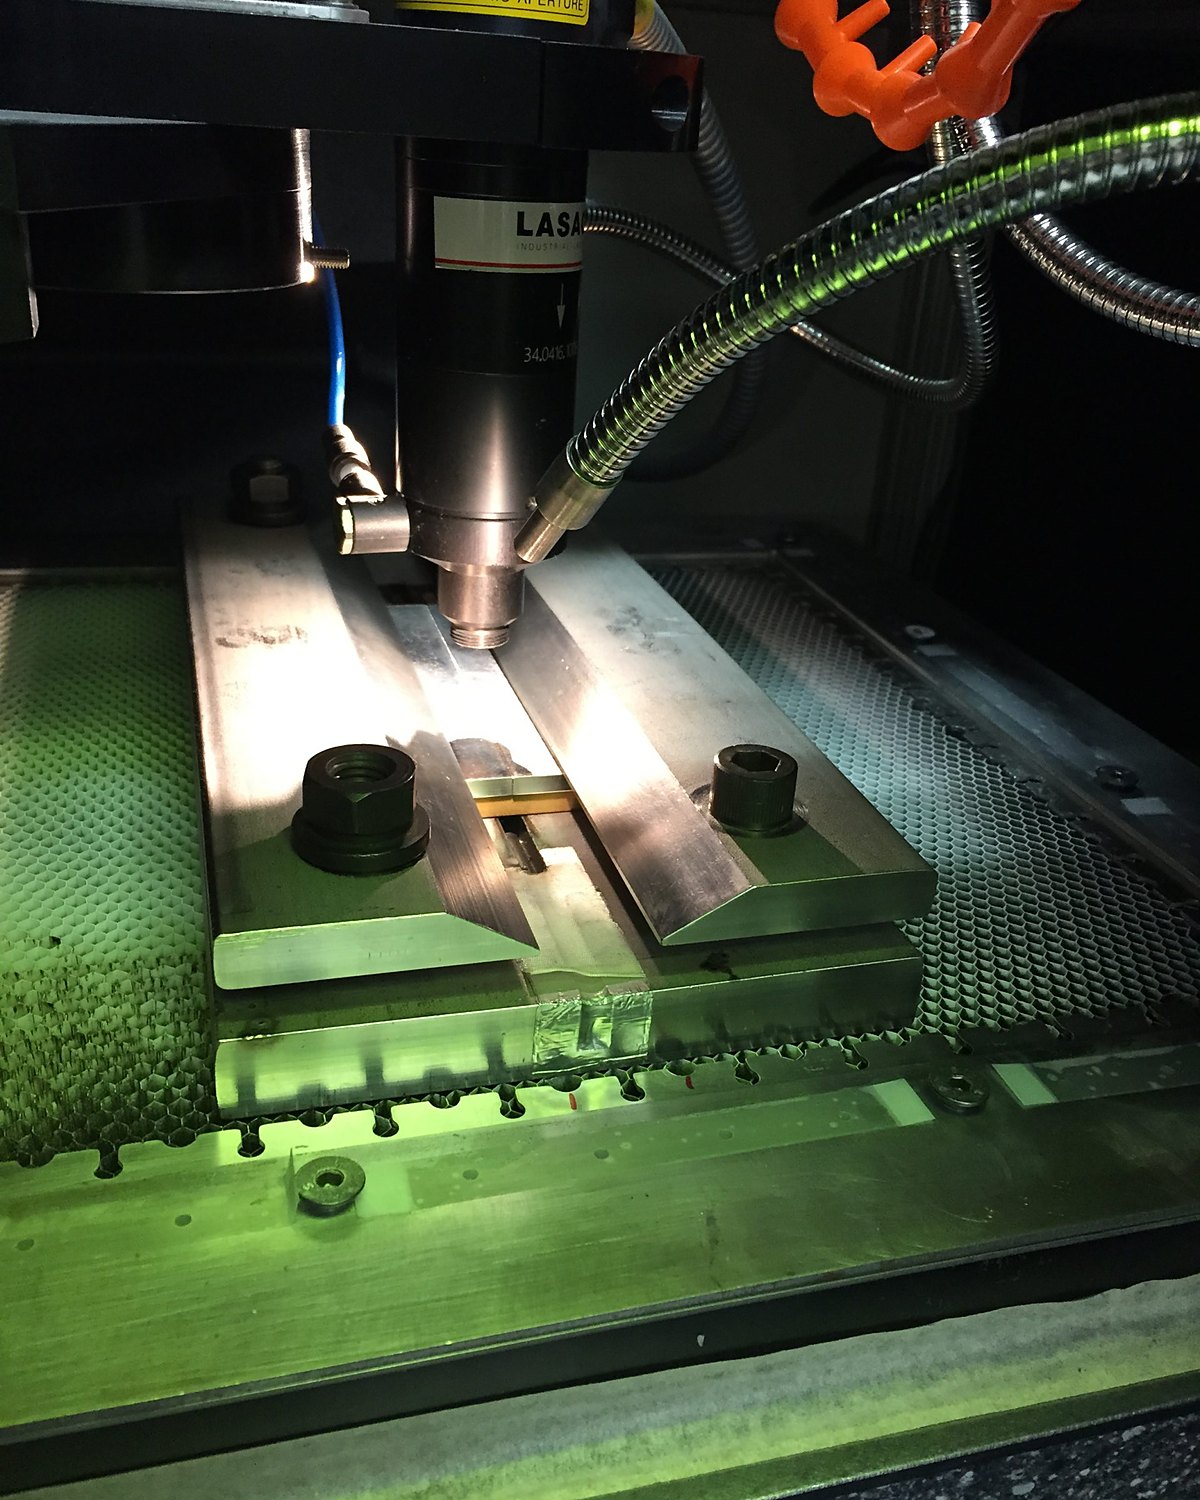
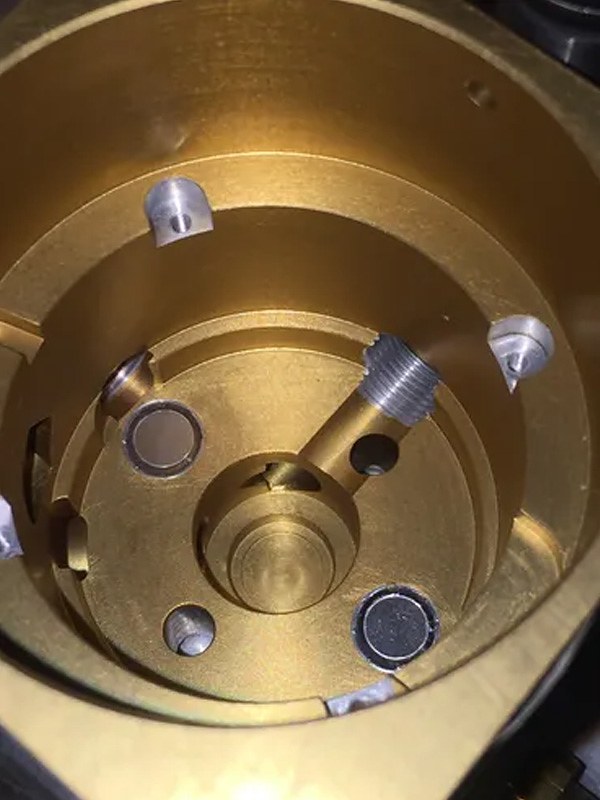
Typical laser welding work
Hermetic sealing
Seam welds on sensor, electronics and battery housings where leak-tight joints are required.
Dissimilar metals
Joints between alloys that are difficult or impossible to join with conventional welding.
Heat-sensitive assemblies
Welds placed next to glass seals, polymers, electronics or finished surfaces.
Micro & spot welding
Precise spot and tack welds on small medical and aerospace components.
Tooling & mold repair
Laser build-up and repair on worn or damaged high-value tooling.
Production runs
Fixtured, repeatable welding from first article through volume production.
Swiss-made LASAG lasers
We use two LASAG sources. Each can shape its laser pulse to get high penetration without cracking the material.
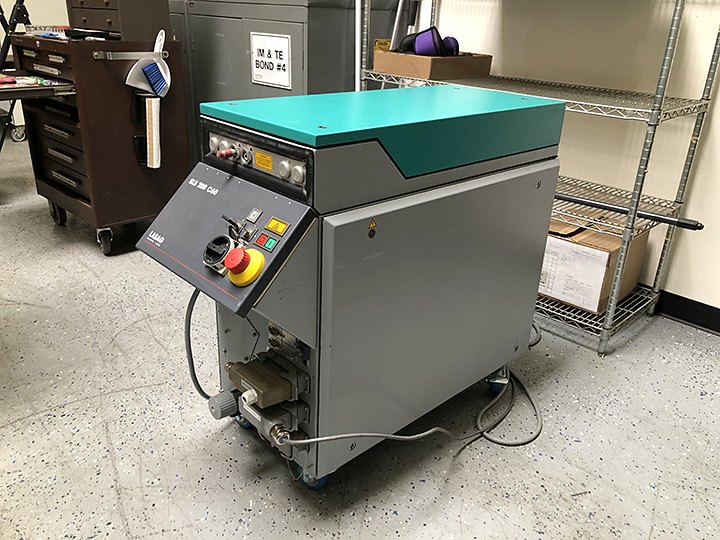
LASAG SLS 200
Delivers the beam through fiber optics, with 10–220 W output for many kinds of welding. A real-time power supply joins identical or dissimilar materials with high quality and repeatability.
- Pulse-to-pulse stability down to ±0.5%
- Long pulses up to 100 ms, high pulse energy, SHADOW® welding
- High-resolution pulse forming, pulse-on-demand and power-burst
- Weld penetration and diameters from 25 to 1000 µm
- Helium- and pressure-tight welds; precision welding of thin foils
- Spot, seam and SHADOW® welding, plus micromachining
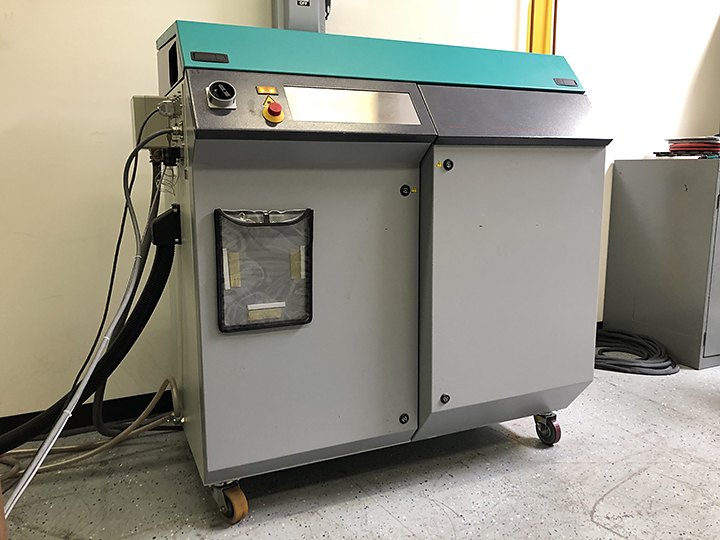
LASAG FLS pulsed Nd:YAG
300–600 W average output, pulse power up to 50 kW and excellent beam quality. Its modular design and adjustable resonator give strong results in cutting, welding, drilling and ablation.
- Seam welding with penetration up to 3 mm and helium-tight welds
- Spot welds ≥ 40 µm diameter
- Single-shot contour welding
- Cuts up to 20 mm thick, kerf width < 20 µm
- Percussion drilling Ø 0.02–1.5 mm, aspect ratio up to 1:30
Key advantages
Laser welding offers high speed, high accuracy, low heat input and low distortion. Fiber-optic beam delivery also allows a high degree of automation.
Low heat input
Energy goes only where it’s needed. That makes welding next to glass-to-metal seals, electronics, O-rings and plastic parts possible, and routine for us.
Clean welds
Clean seams are easier to sterilize and fit into other assemblies without the weld getting in the way.
Strong welds
High strength from a minimum number of welds saves time and improves reliability.
Hermetic welds
Unlike soldering or brazing, laser welding produces flawless hermetic seals, which many medical applications require.
Excellent repeatability
Laser output is very stable, and there are no electrodes to wear or contaminate the weld, so every weld matches the last.
Hard-to-join conductors
Platinum, gold, copper alloys, stainless, Nitinol, titanium, MP35N, Elgiloy and dissimilar metals all weld with excellent, repeatable results.
- Repeatable, high-speed and precise
- Ideal for high production volumes
- Minimal part distortion
- Welds near heat-sensitive parts and hard-to-reach areas
- Consistent depth and width control
- No fluxes or solvents
Controlling every pulse to prevent cracks
A pulsed laser’s peak power overcomes the reflectivity and heat conductivity of aluminum, copper and similar alloys. We shape each pulse over time, adjusting peak power through the pulse to control cooling rates. That reduces cracking, removes porosity, improves how the weld looks, and handles dissimilar metals.
| Ferrous & high-nickel alloys | ≈ 1 kW peak power |
|---|---|
| Aluminum alloys | ≈ 3 kW peak power |
| Copper alloys | ≈ 5 kW peak power |
| Penetration | Up to 3 mm |
Metals & alloys we weld
This includes aluminum alloys, carbon and stainless steels, aircraft alloys, super alloys, electrical steels, titanium, brass, bronze and copper, as well as dissimilar combinations. If yours isn’t listed, ask.
Aluminum alloys
2011 · 2017 · 2024 · 2219 · 5052 · 6061 · 6063 · 6262 · 7050 · 7075 · K100 & more
Carbon steel
1018 · 1025 · 1040 · 1045 · 1112 · 1117 · 1144 · 1215 · 12L14 Ledloy & more
Stainless steel
13-8MO · 15-5PH · 17-4PH · 300/400 series · Nitronic · AM-355 & more
Aircraft alloys
4130 · 4140 · 4330 · 4340 · 4620 · 52100 · 8740 · 9310 · H-11 · Hy-Tuff · Nitriding & more
Super alloys
A-286 · AM350/355 · Hastelloy · Haynes · Hy Mu · Incoloy · Inconel · Maraging · Monel · Nickel · Waspaloy & more
Electrical steels
Invar · Kovar · 4750 & more
Titanium
6Al-4V · 6Al-6V-2Sn · 6Al-7Nb · 8Al-1Mo-1V · 10Al-2V-3Sn · CP 1, 2, 3 & 4 · Ti-1100 & more
Brass & bronze
200/300 series brass · 400/500 series bronze · Ampco · silicon & manganese bronze · aluminum bronze & more
Copper
100 series OFE/OF/ETP/DHP · tellurium copper · half- and full-hard & more
Also processed
Cast iron · coated steels · molybdenum · tantalum · tungsten · zirconium · platinum · gold · Nitinol · MP35N · Elgiloy
Have a drawing ready? Get it reviewed by an engineer.
Send drawings, CAD or photos. An engineer reviews every request.